
 Deutsch
 Español
 Français
 Italiano
 Русский
 简体中文
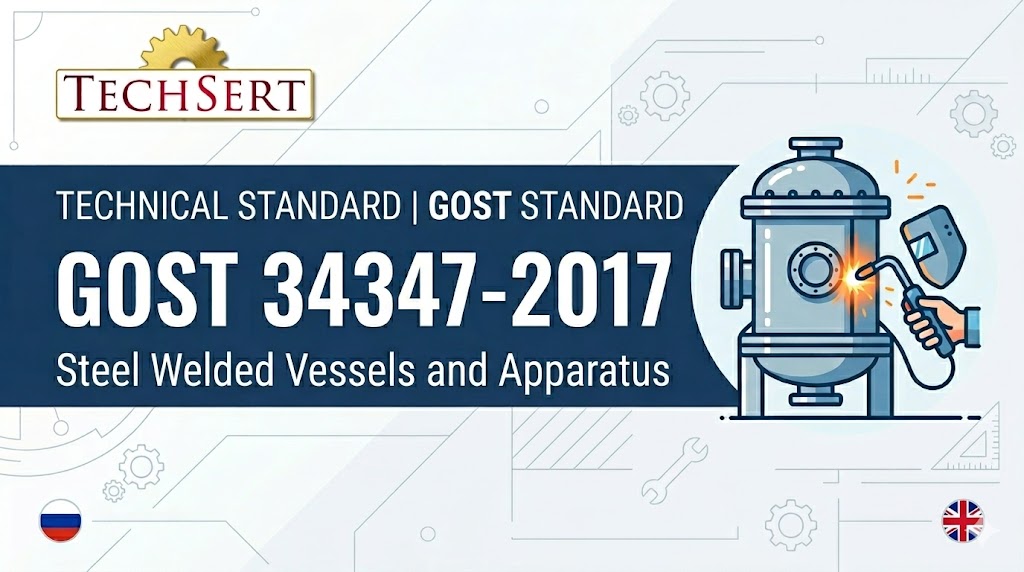
Technical Digest: GOST 34347-2017 – Steel Welded Vessels and Apparatus
GOST 34347-2017 is the primary interstate normative document regulating the design, material selection, fabrication, and testing of steel welded vessels and apparatus within the Eurasian Economic Union (EAEU). It establishes essential safety and operational requirements for equipment functioning under positive gauge pressure, vacuum (residual pressure ≥ 665 Pa), or hydrostatic filling load. Compliance with this standard is mandatory for securing the TR CU 032/2013 EAC Certificate or Declaration.
Download the Complete 2026 Technical Digest
Get the full 5-page English PDF digest containing detailed material equivalence tables (GOST vs. ASTM/EN), exact manufacturing tolerances, comprehensive NDT protocols, and the compliance audit checklist. Fill out the form below to receive the secure download link directly in your inbox.
Gap Analysis: GOST 34347 vs. ASME BPVC Sec. VIII / EN 13445
When harmonizing international designs for EAEU compliance, several critical deviations exist between GOST methodologies and Western codes:
- Classification Architecture: GOST classifies vessels into 5 distinct Groups based on design pressure, design wall temperature, and medium toxicity/explosiveness. ASME relies heavily on “Lethal Service” flags and joint efficiency (E), whereas EN 13445 categorizes by Testing Groups (1 to 4).
- Non-Destructive Testing (NDT): GOST ties RT/UT inspection volumes rigidly to the Vessel Group (e.g., Group 1 & 2 demand 100% inspection). ASME allows designers to select RT volumes (Full, Spot, None) to dictate the joint efficiency multiplier used in wall thickness calculations.
- Geometric Tolerances: GOST imposes highly specific limits on local deformations. For example, edge angularity (peaking) is strictly limited to 0.1s + 3.0 mm (with a hard cap of 5.0 mm for standard shells), requiring customized template checks during fabrication.
| GOST Grade | ASTM / EN Equivalent | Chemical Composition (%) | Mechanical Properties | Temp Range (°C) |
|---|---|---|---|---|
| St3sp | A283 Gr. C / S235JRG2 | C 0.14-0.22, Mn 0.40-0.65 | YS 235 MPa, UTS 370-480 MPa | -20 to 200 |
| 20 | A105 / C22E | C 0.17-0.24, Mn 0.35-0.65 | YS 245 MPa, UTS 410-550 MPa | -20 to 425 |
| 20K | A516 Gr. 60 / P265GH | C 0.16-0.24, Mn 0.35-0.65 | YS 265 MPa, UTS 410-550 MPa | -20 to 475 |
| 16K | A516 Gr. 55 / P235GH | C 0.12-0.20, Mn 0.35-0.65 | YS 235 MPa, UTS 380-470 MPa | -20 to 475 |
| 22K | A516 Gr. 65 / P295GH | C 0.19-0.26, Mn 0.50-0.80 | YS 295 MPa, UTS 430-580 MPa | -20 to 350 |
| 09G2S | A516 Gr. 70 / P355GH | C ≤0.12, Mn 1.30-1.70, Si 0.5-0.8 | YS 345 MPa, UTS 490-620 MPa | -70 to 475 |
| 10G2S1 | A537 Cl. 1 / P355NL1 | C ≤0.12, Mn 1.30-1.65 | YS 345 MPa, UTS 490-620 MPa | -70 to 475 |
| 16GS | A516 Gr. 65 / P295GH | C 0.12-0.18, Mn 0.90-1.20 | YS 295 MPa, UTS 450-590 MPa | -40 to 475 |
| 17GS | A516 Gr. 70 / P355GH | C 0.14-0.20, Mn 1.00-1.40 | YS 345 MPa, UTS 490-620 MPa | -40 to 475 |
| 12MKh | A387 Gr. 12 / 13CrMo4-5 | C 0.08-0.15, Cr 0.4-0.7, Mo 0.4-0.6 | YS 220 MPa, UTS 440-590 MPa | 0 to 540 |
| 15KhM | A387 Gr. 12 / 13CrMo4-5 | C 0.11-0.18, Cr 0.8-1.1, Mo 0.4-0.5 | YS 220 MPa, UTS 440-590 MPa | 0 to 560 |
| 15Kh5M | A387 Gr. 5 / X12CrMo5 | C ≤0.15, Cr 4.5-6.0, Mo 0.45-0.60 | YS 200 MPa, UTS 390-590 MPa | 0 to 650 |
| 08Kh18N10T | 321 / X6CrNiTi18-10 | C ≤0.08, Cr 17-19, Ni 9-11, Ti | YS 205 MPa, UTS 510-730 MPa | -253 to 610 |
| 12Kh18N10T | 321H / X6CrNiTi18-10 | C ≤0.12, Cr 17-19, Ni 9-11, Ti | YS 205 MPa, UTS 510-730 MPa | -253 to 610 |
| 10Kh17N13M2T | 316Ti / X6CrNiMoTi17-12-2 | C ≤0.10, Cr 16-18, Ni 12-14, Mo 2-3 | YS 215 MPa, UTS 510-730 MPa | -253 to 700 |
Strict numerical limits are placed on fabrication to prevent structural anomalies:
- Length Deviation: Permitted up to ±0.3% of the nominal length, capped at a maximum of ±50.0 mm.
- Straightness: Cannot exceed 2.0 mm per 1 meter of length, capped at 30.0 mm for vessels exceeding 15 meters.
- Relative Ovality: Maximum 1.0% for standard pressure vessels; restricted to 0.5% for vessels under vacuum/external pressure; allowed up to 2.0% for filling-only vessels.
- Edge Misalignment (Offset): For longitudinal welds up to 20.0 mm thickness, offset is limited to 0.1s (max 3.0 mm). For circumferential welds, it is limited to 0.1s + 1.0 mm.
Non-Destructive Testing volumes are strictly mandated based on the vessel’s designated Group:
- 100% Visual & Measuring Control (VT): Mandatory for all welds prior to any internal inspection.
- Groups 1 & 2: 100% RT (Radiographic) or UT (Ultrasonic) testing of butt, corner, and T-joints.
- Group 3: 50% RT or UT of applicable welds.
- Group 4: 25% RT or UT of applicable welds.
- Group 5: 10% RT or UT of applicable welds.
- Penetrant/Magnetic Particle Testing (PT/MT): Mandatory for all welds inaccessible by RT/UT, and for steels highly prone to cracking (e.g., martensitic or austenitic non-ferritic steels).
EAC and Gost Certification News

Exporting to Russia 2026: Strategic Non-Sanctioned Key Sectors
Many businesses, large and small, have a huge source of great ideas that can help them improve, innovate, and grow, and yet so many of these companies never think of using this amazing corporate asset. What is this highly valuable asset? Its own people.
10 March 2026
EAC Certificate or Declaration? The Complete 2026 Guide to Eurasian Compliance
Many businesses, large and small, have a huge source of great ideas that can help them improve, innovate, and grow, and yet so many of these companies never think of using this amazing corporate asset. What is this highly valuable asset? Its own people.
10 February 2026
The EAC certifications for the Oil & Gas sector in the Eurasian Economic Union
Many businesses, large and small, have a huge source of great ideas that can help them improve, innovate, and grow, and yet so many of these companies never think of using this amazing corporate asset. What is this highly valuable asset? Its own people.
27 October 2025Mandatory sample importation for EAC certifications
Many businesses, large and small, have a huge source of great ideas that can help them improve, innovate, and grow, and yet so many of these companies never think of using this amazing corporate asset. What is this highly valuable asset? Its own people.
10 April 2019
EAC and Gost Certifications by Product

china@gostrussia.com
india@gostrussia.com
+44 203 630 13 04
+49 891 437 75 12
8 800 500 31 57
+39 02 947 509 21
+34 911 798 351